A facility that comes back to the same conveyor manufacturer for a second project isn’t making a loyalty decision. They’re making a risk management decision. They’ve already seen how the engineering held up, whether the delivery timeline was real, and what happened when something needed to be adjusted after commissioning.
Repeat business in industrial conveyor supply doesn’t come from a good sales pitch; it comes from systems that performed the way they were specced. The first project is where a manufacturer shows you the proposal. The second is where you find out what the proposal didn’t cover. How they handled the spec assumption that turned out to be wrong.
Whether the parts were available when something needed replacing. Whether the timeline held when the project hit friction. That’s what conveyor manufacturer experience looks like from the outside. Not a founding date on a website, not a list of industries served, but a pattern of customers who had options and kept coming back.
What Experience Buys You That a Proposal Can’t Show
A spec sheet can look identical coming from a shop that opened four years ago and one that’s been building systems for decades. The difference doesn’t show up in the quote. It shows up six months after commissioning, when a roller spec that didn’t account for actual load distribution starts causing jams, or a drive configuration that worked on paper creates timing issues with upstream equipment.
Experienced manufacturers catch those problems during engineering because they’ve seen them before. Not versions of them, but the actual failure mode on a similar application in a comparable facility. That reference library doesn’t appear in a proposal, but it shapes every decision that does.
Rolmaster maintains a database of thousands of prior standard and custom designs, which means the engineering team isn’t treating your application as novel when it isn’t. A configuration that looks unique in your facility has usually shown up in some form before, and the lessons from that prior version get applied before your system goes into production, not after the first fault report lands on someone’s desk.
Less Time Spent Reinventing the Wheel
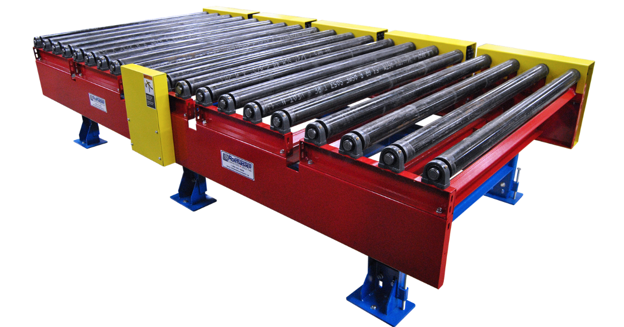
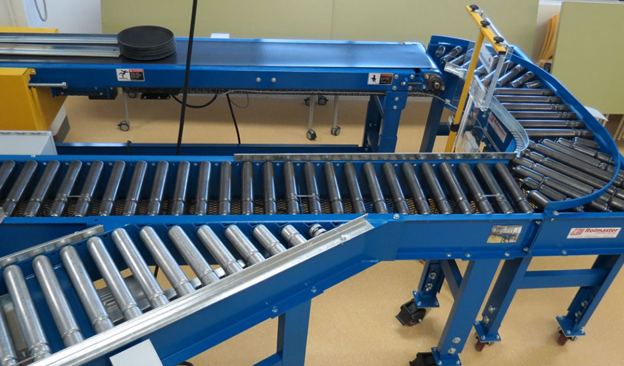
Conveyors can look fairly simple from the outside. You have a frame, rollers or belting, a drive system where required, and a product that needs to move from one location to another.
The details are where things get complicated.
How heavy is the product? Where is that weight concentrated? What’s the smallest product being conveyed? How frequently will the conveyor start and stop? Are products accumulating? What happens at the transfer points? How much space is available? What conditions will the conveyor be operating in?
Even something as basic as roller spacing can become important when you’re dealing with a wide range of product sizes. An experienced conveyor manufacturer has dealt with these questions before. In many cases, they’ve dealt with them hundreds of times.
That doesn’t mean every application gets the same solution. It means there is already a starting point.
Instead of designing every system from scratch, previous applications can help determine what makes sense and, equally importantly, what doesn’t.
Where Conveyor Vendor Selection Goes Wrong
Most conveyor vendor selection processes weight price heavily and track record lightly. That’s defensible when the budget conversation happens in Q2 and the commissioning problems arrive in Q4 — they don’t land on the same desk at the same time. The person approving the purchase order isn’t usually the person troubleshooting the timing fault eight months later.
The costs that don’t appear in the original quote: extended commissioning, production downtime during calibration, retrofit work when a spec assumption turns out to be wrong, and the staff hours spent managing a deteriorating vendor relationship. A heavy-duty conveyor selection guide that accounts for these downstream factors changes what “lowest bid” means when you run the full numbers.
Assembly Magazine reported on a Senseye study that found large manufacturers lose an average of 27 hours per month to equipment failures. In automotive plants specifically, that figure climbs to 29 hours monthly at a cost of $1.3 million per hour.
That’s the actual cost environment in which a conveyor vendor decision sits. The capital difference between a lower-priced quote and a well-specced system from an experienced manufacturer closes fast once you factor in the first unplanned stoppage.
What Proven Conveyor Systems Look Like After Five Years
A proven conveyor system isn’t one that worked at installation. It’s one that’s still performing within spec after years of production cycles, shift changes, and the incremental loading creep that happens when a line gets busier than the original design assumed.
Modern Materials Handling puts the operational life expectancy of a well-designed conveyor system at 15 to 20 years. Whether a system reaches that is largely determined by decisions made before fabrication starts: roller diameter selection, bearing specification, drive configuration, load rating assumptions.
An experienced manufacturer builds margin into those decisions based on what they’ve seen fail. A newer shop builds to the spec as written, which is technically correct and sometimes insufficient.
Consider how load ratings work in practice. CDLR capacity ratings assume even load distribution across rollers. Concentrated weight on individual contact points, which happens regularly with certain pallet configurations, creates failure conditions under loads that should be within spec. Catching that during engineering requires having seen it fail. It’s not in any manual.
Canadian conveyor manufacturers also deal with operating conditions that offshore suppliers and newer domestic shops tend to underestimate. Temperature swings between a January loading dock and a heated production floor affect bearing lubrication in ways that don’t show up until the second winter. A manufacturer operating in Ontario understands this without being told — it’s already accounted for in how systems get specced.
Mistakes Are Much Cheaper on Paper
One of the most expensive times to discover a design problem is after the equipment has been installed.
Maybe the smallest product doesn’t transfer properly. Maybe a component wears faster than anticipated. Perhaps the drive works fine when the conveyor is empty but struggles during repeated starts with a full load. None of these problems necessarily mean the original design was unreasonable. Some problems only become obvious through experience.
A manufacturer that has been building similar equipment for years has had the opportunity to see those situations play out. That knowledge gets carried into future projects. Sometimes it’s a major design decision. Other times it’s something small: changing a roller center, selecting a different bearing, increasing a shaft size, moving a drive location, or providing a little more clearance somewhere. On a drawing, the difference might seem insignificant.
Five years into the conveyor’s working life, it might not be insignificant at all.
Downtime Changes the Cost Equation
Purchase price is easy to measure. Downtime isn’t. If a conveyor on a critical production line goes down, the original purchase price quickly becomes irrelevant.
People may have to move material manually. Production can slow or stop. Maintenance personnel get pulled away from other work. Somebody has to identify the failed component, find a replacement and get the equipment running again. Depending on the operation, a few hours of downtime can easily cost more than the difference between two original equipment quotes.
That’s why maintainability and parts availability matter.
A conveyor designed around proven components, with a manufacturer that can identify what was originally supplied, can make troubleshooting and repairs considerably easier. You don’t really appreciate that advantage when the conveyor is running. You appreciate it when it isn’t.
The Supply Chain Behind the Quote
A manufacturer with decades of operating history has supplier relationships that a newer shop doesn’t. Rolmaster works with over 2,200 supply chain partners. That network affects lead times, parts availability, and the ability to source components when a standard supplier has an interruption, which happens more often than procurement teams plan for.
This matters most when something needs to be replaced under production pressure. A conveyor roller measurement and replacement guide helps facilities identify what they need quickly, but having the supply chain depth to fulfill that request without a multi-week wait is a separate capability. It takes years to build and can’t be replicated by a newer entrant offering a competitive price on the initial system.
Parts availability also affects how a manufacturer responds when a design issue surfaces post-commissioning. A shop with deep supplier relationships can source a modified component and get a corrected part to the facility without the project stalling for weeks. A thinner supplier base doesn’t offer the same options, and the facility waiting on the fix absorbs the delay.
Rolmaster’s 90% on-time delivery rate reflects both conveyor manufacturer experience, capacity, and supply chain depth. These cannot exist without the operational history to develop them.
The Benefits of an Established Manufacturer in Practice
The benefits of an established manufacturer aren’t abstract. They show up in specific moments: when an engineer recognizes a load distribution problem before fabrication starts, when a parts request gets filled without halting a production line, when a system commissioned five years ago still runs within original spec because the bearing selection had a real-world margin built in.
They also show up in what doesn’t happen: the retrofit caught on paper, the bearing failure designed around, the commissioning delay that never materialized because someone had seen that configuration fail before.
They also show up when something goes wrong. An established manufacturer has encountered enough post-commissioning issues to know which are installation variables and which are design problems. That distinction matters when you’re trying to resolve a fault quickly and need someone who can tell the difference without a lengthy back-and-forth. The faster the diagnosis, the less production time is lost waiting for an answer.
Long-term conveyor supplier relationships tend to form around this kind of accountability. Facilities that recognize the signs a conveyor system needs attention early enough to plan a replacement rather than react to a failure are usually working with a manufacturer they trust to give them an honest assessment — not one trying to protect a first sale.
There’s Value in Equipment That’s Already Proven Itself
New technology has an important place in manufacturing, but not every application requires a completely new solution. There is a lot to be said for equipment that has already spent years working in actual plants.
If a manufacturer has been producing a particular conveyor or roller design for a long time, there is real-world history behind that design, and it is considered to be a proven conveyor system. It has been fabricated repeatedly, installed in different applications, maintained by different crews and subjected to conditions that are difficult to duplicate during a short test.
Over time, manufacturers learn from that history. Designs change. Components improve. Problems that showed up on earlier equipment can be corrected on later versions. Eventually, what looks like a fairly simple conveyor can represent years of small improvements. That’s difficult to put on a specification sheet, but it matters.
Custom Equipment Benefits From Experience Too
Custom manufacturing isn’t just about being able to build something unusual. It’s knowing what actually needs to be custom.
Making every component unique can create problems of its own. Costs increase, manufacturing becomes more complicated, and replacement parts become harder to source.
A good custom design keeps proven components wherever they make sense and changes the areas that actually need to change. For example, a conveyor might require an unusual frame width or elevation while still being able to use an established roller design. A drive arrangement might need to change without requiring an entirely new conveyor platform.
Those decisions aren’t always obvious. Experience helps a manufacturer recognize where customization adds value and where it simply adds complexity.
What a New Vendor Can’t Compress
A newer Canadian conveyor manufacturer can hire experienced engineers, invest in equipment, and price aggressively to win business. What they can’t compress is accumulated project history. That tells you a particular configuration creates transfer point problems when load weights vary, or that a bearing spec that looks fine on paper under-performs once the temperature drops.
That knowledge doesn’t live in a manual. It lives in the engineers who specced the system that failed that way, corrected it, and carried the lesson into every subsequent project. There’s no shortcut to it. You either have the project volume to have encountered the failure, or you haven’t, and the facility absorbing the cost of a first-time mistake is rarely the one that knew they were taking that risk. That’s why conveyor vendor selection is so important for manufacturing facilities, and why they tend to stick with the same vendors over time – a proven track record is extremely important in the business of conveyors.
Replacement Parts Are Where History Really Pays Off
A conveyor doesn’t stop being the manufacturer’s concern just because it has shipped.
At least, it shouldn’t.
Industrial equipment can remain in service for decades. During that time, parts are going to wear out. Rollers will eventually need replacing. Bearings can fail. Sprockets wear. Motors and gearboxes don’t last forever. The question then becomes: can anyone still figure out what you bought? This is an area where dealing with a long-term conveyor supplier can make a noticeable difference.
If previous orders, drawings and component specifications have been maintained, an old conveyor doesn’t necessarily have to be reverse-engineered every time something needs replacing. Being able to trace equipment back to an original order can turn a lengthy investigation into a much simpler conversation. For a maintenance department dealing with a conveyor that’s holding up production, that difference matters considerably more than it did when somebody was comparing quotes years earlier.
The Feedback Loop a Newer Shop Can’t Buy
At Rolmaster, that institutional memory goes back to 1946, through ownership changes, acquisitions, and 80 years of Canadian manufacturing conditions that have a way of exposing assumptions that looked solid in an engineering drawing.
That history isn’t stored in a document; it’s carried by the engineers who worked through the failures, adjusted the specs, and applied what they learned to the next project. Each decade adds another layer of application knowledge that a newer shop simply hasn’t had time to accumulate.
The feedback loop between what gets designed and what gets reported back from the field is short. A configuration that causes problems in January gets corrected in February. That correction gets built into the engineering defaults.
The next facility with a similar application benefits from it without knowing it existed. That only happens when you have enough project history to encounter the failure, recognize the pattern, and close the loop before the next system ships.
When a facility is evaluating vendors, the question isn’t whether the newer shop can build a conveyor. They probably can. The question is what happens when the project hits friction, and whether the manufacturer on the other end of that call has been close enough to this specific problem to say something useful.
If you’re at that stage in a procurement decision, our Cambridge team is available at info@rolmasterconveyors.ca to work through your load requirements, operating conditions, and what a realistic system spec looks like for your application. You will receive the premier conveyor manufacturer experience with Rolmaster.